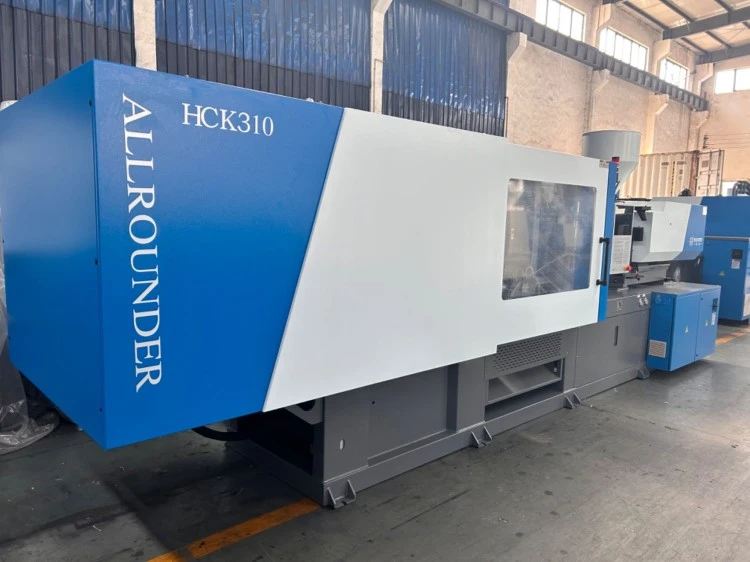
Mold quality and well-organized trial runs are critical for us—they directly affect product qualification rate, production efficiency, and overall cost control.
We selected a standard fruit crate as our research model:400×450×120mm, made of PP raw material, and has a net weight of 340g.
We share Haichen’s full crate mold workflow in this article.
Then, we design molds and test them on our HCK310 injection molding machine.
We also sum up and embed key operational tips into every production step, helping both us and our customers achieve stable, cost-efficient mass production.
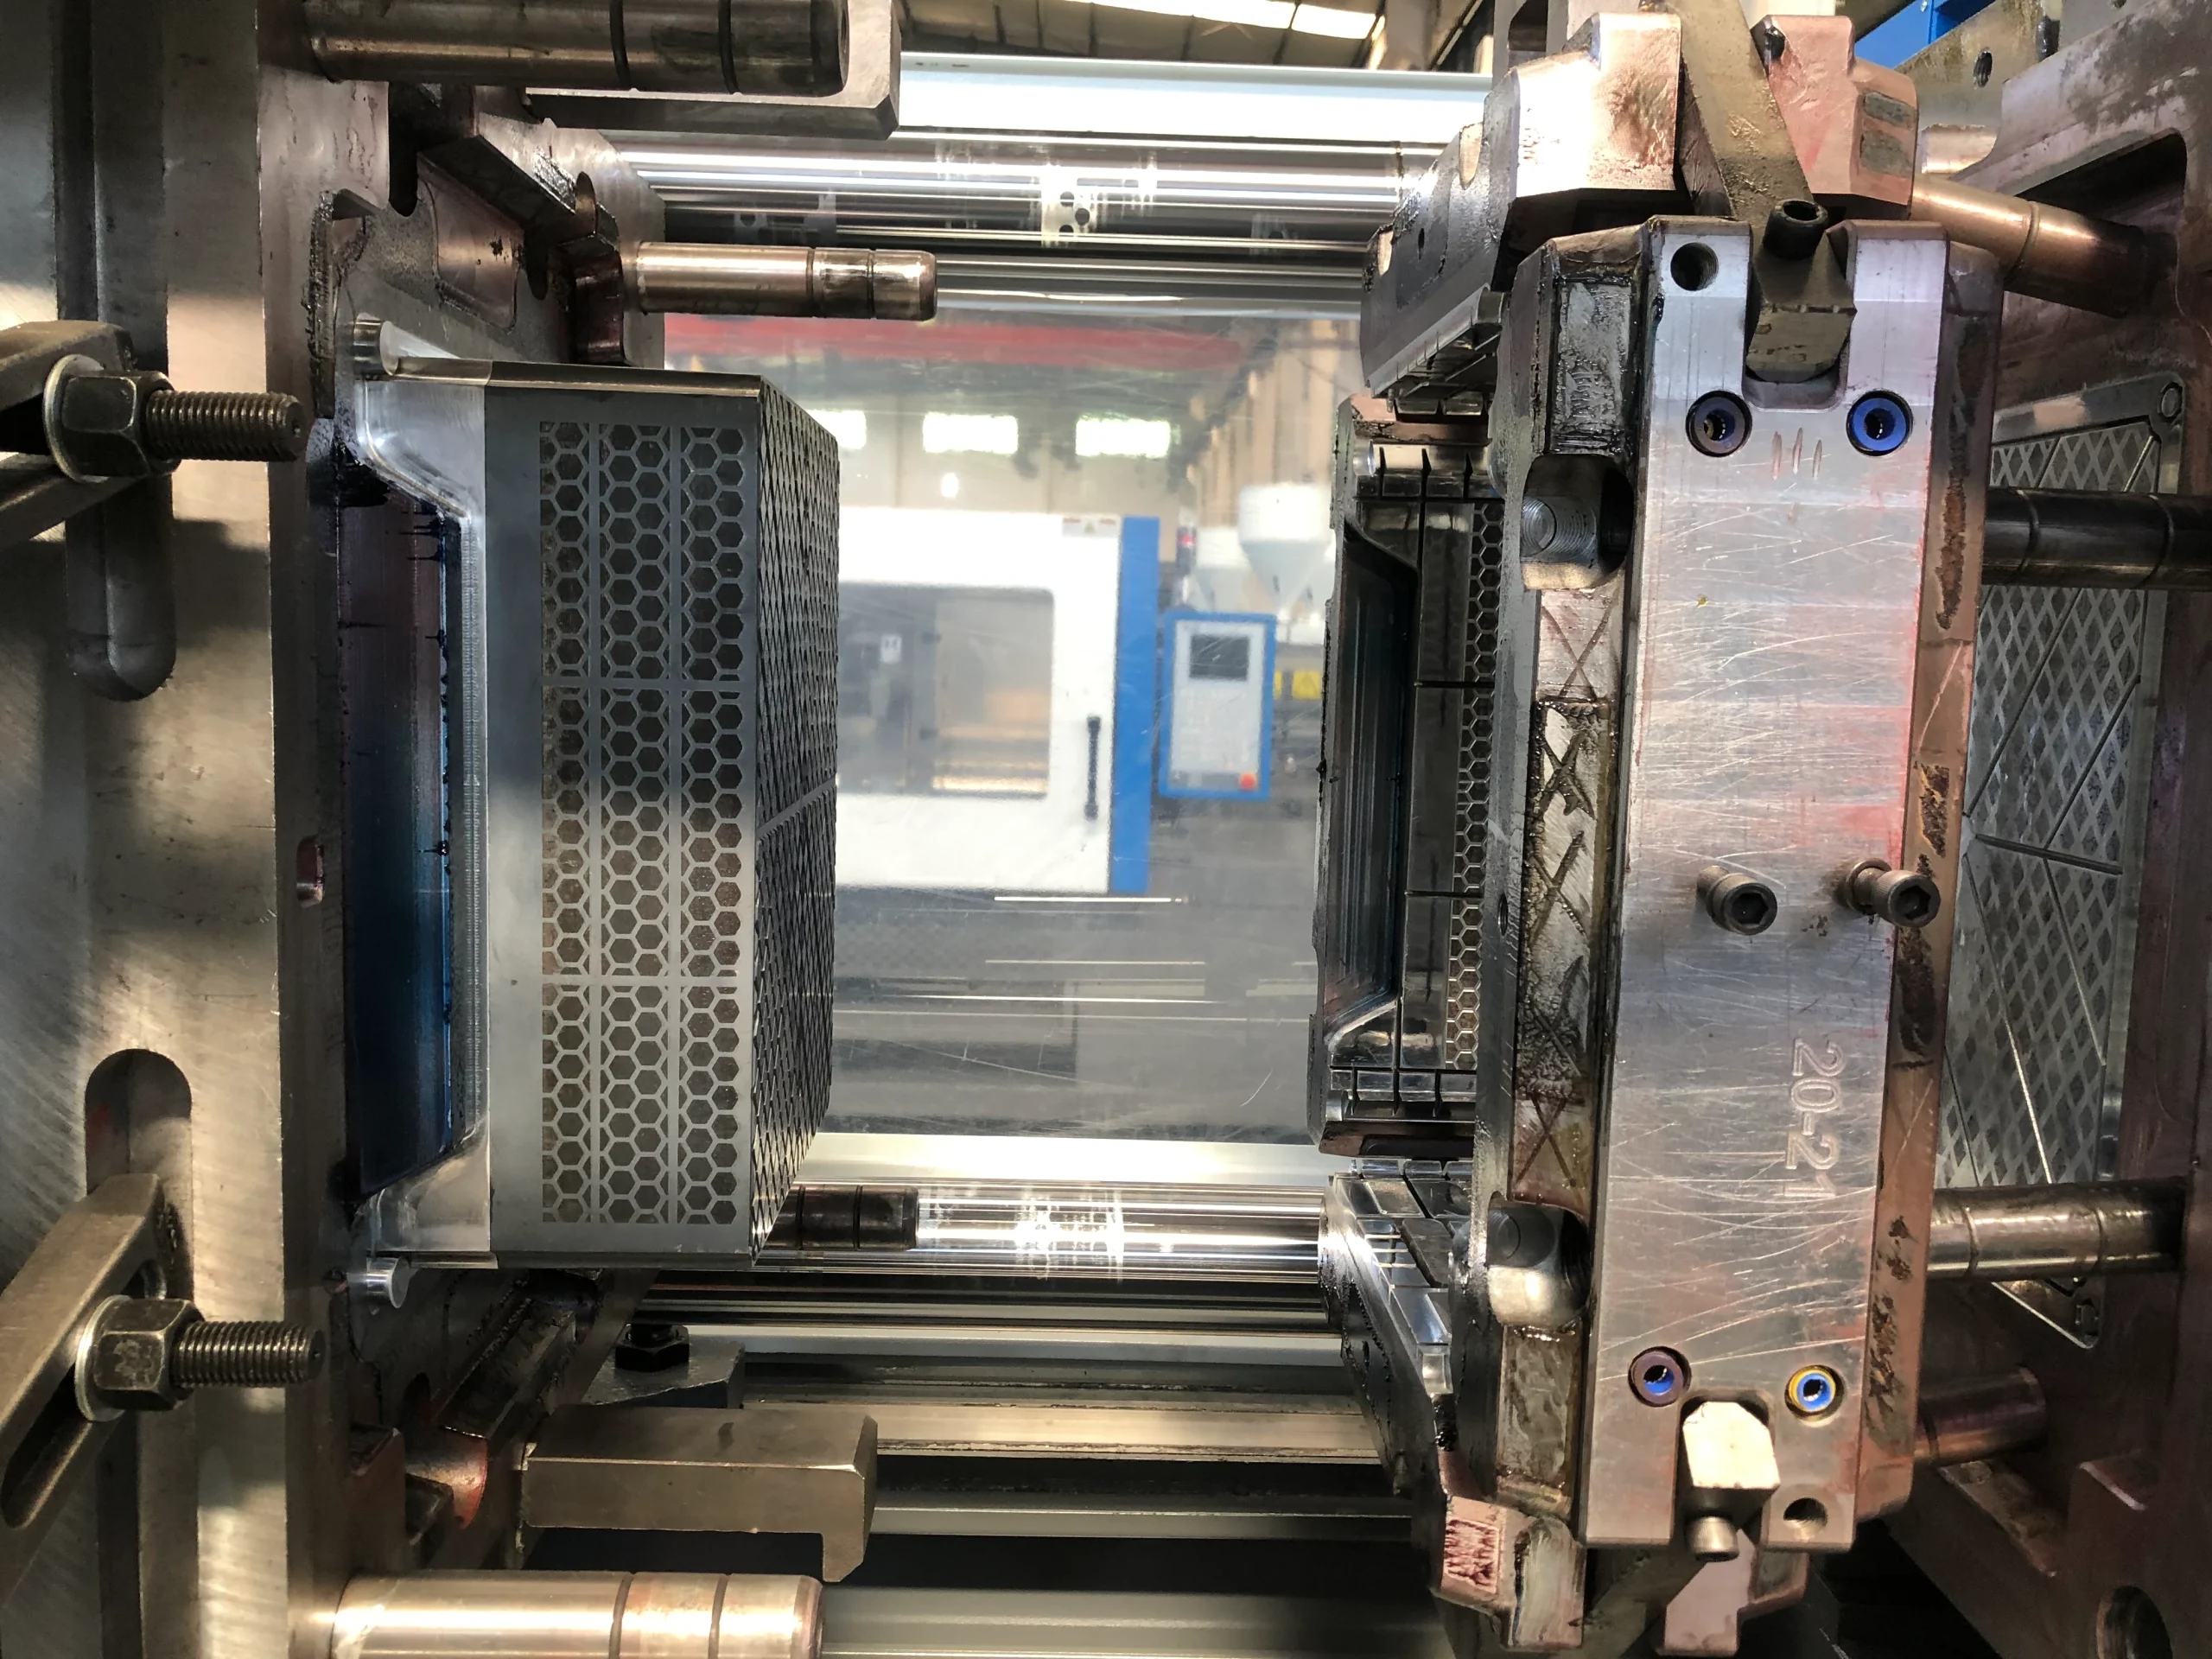
Mould Structure
The mould structure mainly includes cavity, core, gating system, cooling system, demolding system and guide mechanism.
Combined with the use requirements of Haichen HCK310 injection molding machine emphatically.
Also the mold structure design fully considers the adaptability to the machine’s tie rod spacing and maximum mold thickness.
In view of the need to control flash during injection, the outer edge of the mold cavity is designed in strict accordance with the 14cm safety standard.
Which cooperates with the stable clamping force of the Haichen HCK310 machine to avoid flash defects caused by insufficient mold sealing.
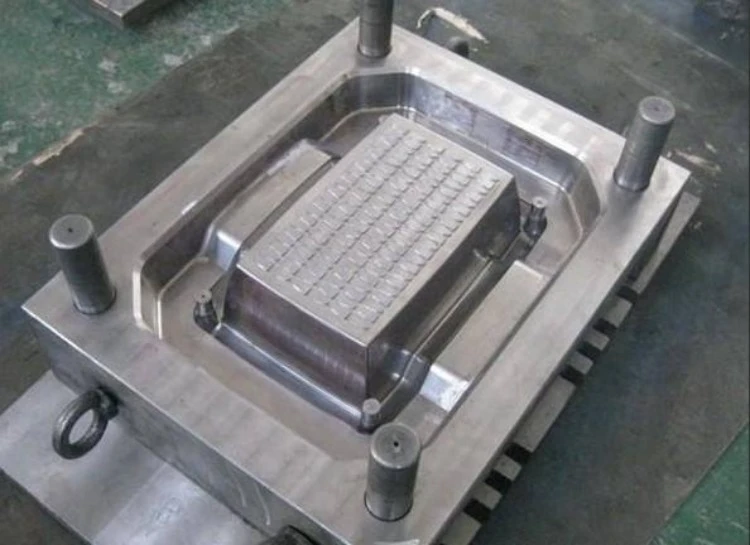
Plastic Crate & Mold Design
- 3D CAD Model
- Material Selection
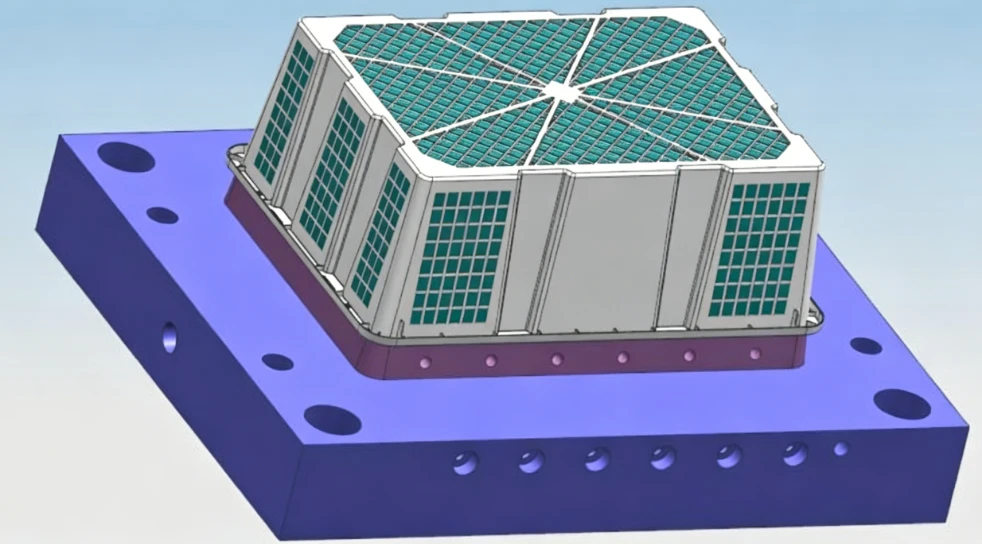
3D CAD Model
The 3D CAD model design is the foundation of mold manufacturing and product forming, which needs to comprehensively consider product size, material characteristics, mold-machine matching and cost control.
First, according to the 400*450*120mm size requirement of the fruit crate, the 3D model of the product is established, and the wall thickness is reasonably designed.
Since the product is made of PP material and needs to be thin and light to save raw materials, the wall thickness is controlled at 1.5-2.0mm, which is close to the concept of thin-wall.
Material Selection
For mould materials, considering the production volume and cost, P20 steel is selected as the cavity and core material.
Which has good machinability and wear resistance, and can meet the production needs of disposable crates.
After heat treatment, the hardness can reach HRC28-32, which can effectively resist the wear caused by PP material injection.
The mold base adopts standard LKM mold base, which is compatible with the installation size of the Haichen HCK310 injection molding machine.
Then ensuring that the mold can be accurately installed and positioned on the machine.
At the same time, the mold guide pins and guide sleeves are made of high-hardness alloy steel, which improves the guiding accuracy and service life of the mold.
And cooperates with the stable operation of the Haichen HCK310 machine to ensure the consistency of product size.
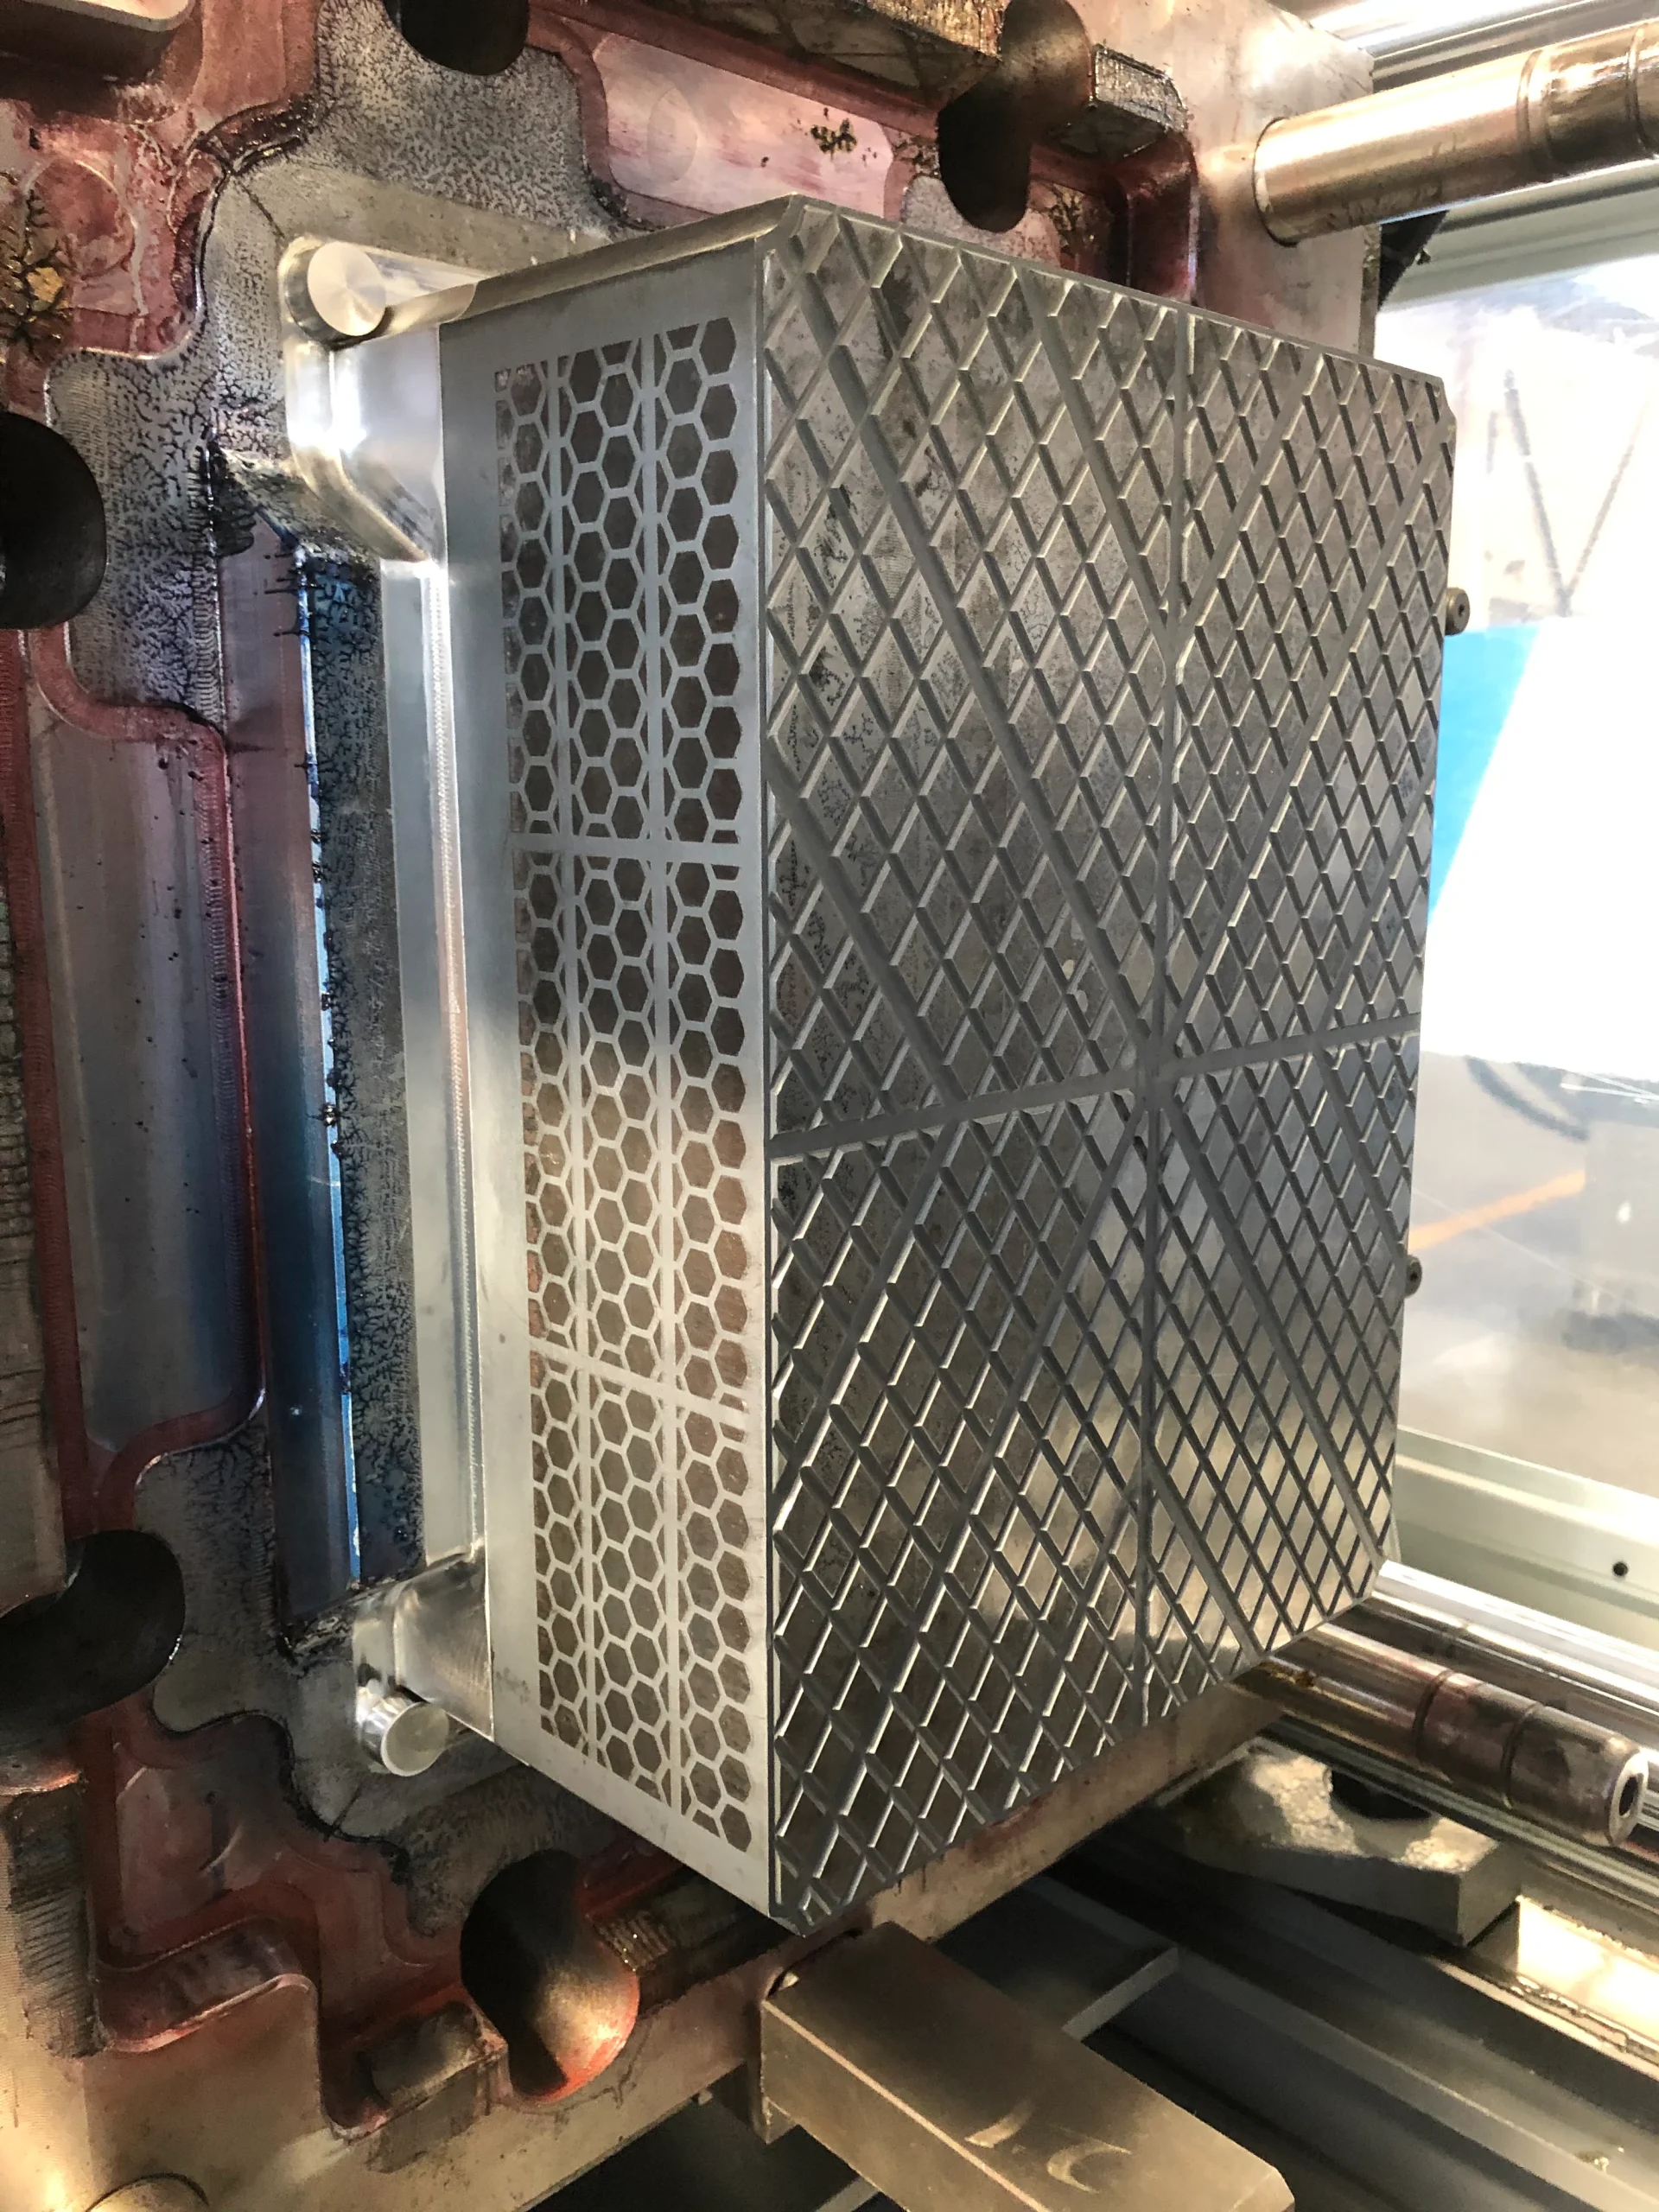
Plastic crate Mould Manufacturing
- CNC Machining
- EDM/Wire Cutting
- Heat Treatment
- Surface Finishing
- Assembly
CNC Machining
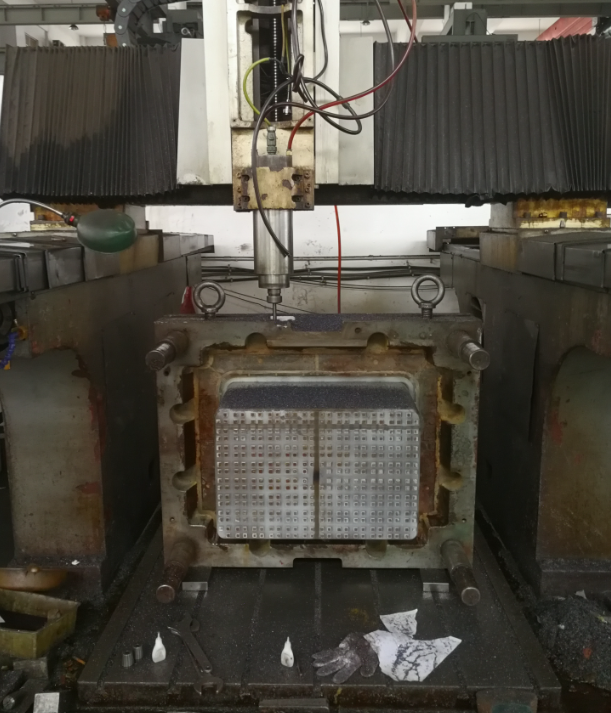
CNC machining is the core link of mold manufacturing, which directly determines the dimensional accuracy and surface quality of the mold.
In the rough machining stage, a milling machine or CNC machine is used to remove a large amount of margin, and a margin of 0.2-0.5mm is reserved on one side also.
In the finishing stage, a high-precision CNC machine is used to achieve a tolerance of 0.005-0.01mm.
Basically,it is used for key parts such as the cavity and gate to ensure the surface roughness and dimensional accuracy of the mold.
At the same time, the thickness of the mold is strictly controlled to ensure that it is within the maximum mold thickness range of the Haichen HCK310 machine, so that the mold can be installed normally.
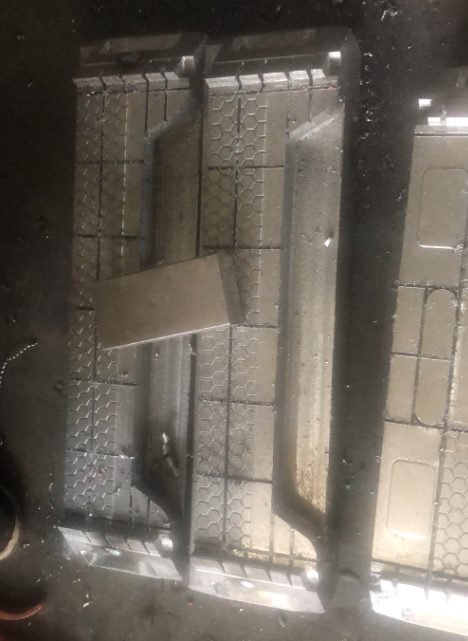
EDM/Wire Cutting
EDM (Electrical Discharge Machining) and Wire Cutting are mainly used to process complex and high-precision structures in the mold that are difficult to process by CNC machining.
Such as small holes, narrow slots, and complex contours of the cavity.
Then,for the mold of the 400*450*120mm fruit crate, wire cutting is used to process the fine structure of the cavity and core.
Such as the gap of the reinforcing ribs and the precision structure of the honeycomb periphery, to ensure the dimensional accuracy of these parts.
Heat Treatment
Generally,Heat treatment is an important link to improve the hardness, wear resistance and service life of the mold.
The mold parts (cavity, core, guide pins, etc.) after CNC machining and EDM/Wire Cutting need to go through strict heat treatment processes, including quenching, tempering and annealing, to eliminate internal stress and improve the mechanical properties of the material.
Then after heat treatment, the hardness of the cavity and core reaches HRC28-32.
Which can effectively resist the wear caused by the injection of PP material.
And avoid mold deformation during the high-temperature and high-pressure injection process of the Haichen HCK310 machine.
At the same time, the heat treatment of the mold parts also needs to ensure the dimensional stability of the mold.
So that the mold can maintain high precision during long-term production.
Then cooperate with the Haichen HCK310 injection molding machine to produce qualified products stably chiefly.
Surface Finishing
Acutally,surface finishing of the mold mainly includes polishing and texturing, which directly affects the surface quality of the fruit crate and the smoothness of demolding.
This not only ensures that the surface of the fruit crate is smooth and free of burrs.
But also reduces the friction between the product and the mold, which is conducive to demolding and improves production efficiency.
After surface finishing, the mold surface is clean and smooth.
Which can effectively prevent the PP material from adhering to the mold during injection, reduce the use of release agent.
And cooperate with the demolding system of the Haichen HCK310 injection molding machine to realize smooth demolding.
Assembly
Then mold assembly is the final link of mold manufacturing, which requires accurate assembly of all mold parts to ensure the normal operation of the mold.
Before assembly, clean all mold parts to remove oil and debris, and apply lubricating oil to guide pins and guide sleeves for smooth operation.
Follow the mold assembly drawing strictly throughout the assembly process, and control assembly accuracy to keep the fit gap of all components within the design range.
Also oay special attention to installing the demolding system and gating system during assembly.
Mount the ejector plate, ejector pin and other demolding components precisely to maintain even ejection force.
Then this prevents product deformation or damage during demolding. Install the gating system smoothly so PP melt flows evenly into the mold cavity.
Overall Complete air tightness and flexibility tests on the assembled mold.
In brief,check mold thickness and installation dimensions to match the Haichen HCK310 injection molding machine.
Reinspect the outer edge of the mold cavity to comply with the 14 cm safety standard and prepare for subsequent trial operation.
Haichen Injection Molding Machine & crate Mold installation
- Machine Selection
- Mold Installation
Machine Selection
According to the parameters of the fruit crate (400*450*120mm, PP material, 340g weight) and the characteristics of the single-cavity mold, the Haichen HCK310 injection molding machine is selected.
Which has the advantages of stable performance, high precision and energy saving.
And is very suitable for the production of small and medium-sized plastic crates.
The Haichen HCK310 injection molding machine has sufficient clamping force (up to 3100kN) and injection pressure (up to 175MPa).
Which can fully meet the injection requirements of thin-walled PP products.
| HAICHEN HCK310 Injection molding machine | |||||
| 说明 | DESCRIPTION | UNIT | |||
| 国际公认型号 | international size rating | 1900 | |||
| 射胶系统 INJECTION UNIT | A | B | C | ||
| 螺杆直径 | mm | 60 | 65 | 70 | |
| 螺杆长径比 | Screw L:D ratio | 21.7 | 20.0 | 18.6 | |
| 理论注射容积 | Shot volume | cm3 | 919 | 1078 | 1251 |
| 实际注射量 | Shot weight(PS) | g | 836 | 981 | 1138 |
| oz | 29.5 | 34.6 | 40.1 | ||
| 射胶压力 | Injection pressure | Bar | 2078 | 1771 | 1527 |
| 注射速率 | Injection rate | cm3/s | 281 | 330 | 383 |
| 注射速率 | Injection rate(acc) | cm3/s | 281 | 330 | 383 |
| 塑化能力 | Plasticizing capacity | g/s | 42 | 51 | 60 |
| 注射行程 | Injection stroke | mm | 325 | ||
| 注射速度 | Injection speed | mm/s | 109 | ||
| 螺杆最大转速 | Max.screw speed | r/min | 200 | ||
| 锁模系统 CLAMPING UNIT | |||||
| 锁模力 | Clamping force | kN | 3100 | ||
| 拉杆内间距 | Space between tie bars | mm | 670×620 | ||
| 模板外形 | mm | 950×880 | |||
| 锁模行程 | Opening stroke | mm | 610 | ||
| 最小模厚 | Min.mold height | mm | 270 | ||
| 最大模厚 | Max.mold height | mm | 670 | ||
| 模板最大距离 | Distance between platens(daylight) | mm | |||
| 顶出行程 | Ejector stroke | mm | 170 | ||
| 顶出力 | Ejector force | kN | 90 | ||
| 顶出杆数 | Number of ejector | 13 | |||
| 动力/电热 POWER UNIT | |||||
| 油压系统压力 | Systerm pressure | Bar | 175 | ||
| 油泵马达功率 | Pump motor | kW | 38 | ||
| 电热功率 | Heating capacity | kW | 20.0 | ||
| 温度控制区 | Number of temp zones | 5+1 | |||
| 其它 GENERAL | |||||
| 干循环时间 | Dry-cycle time | s-mm | 2.8-390 | ||
| 油箱容量 | Oil tank capacity | L | 400 | ||
| 外形尺寸 | Machine dimension(L×W×H) | m×m×m | 6.5×1.6×2.3 | ||
| 机器重量 | Machine weight | t | 9.7 | ||
| 料斗容积 | Hopper capacity | kg | 50 | ||
Mold Installation
Mold installation is critical for stable injection molding machine operation and qualified product quality.
Before installation, inspect the Haichen HCK310 machine and mold.
Check the machine’s running status and the integrity of tie rods and platens; check the mold for cracks and deformation.
Then its installation dimensions match the machine, and confirm the cavity outer edge meets the 14 cm safety standard.
Finally,clean the mold and machine platens to clear oil and debris, and align the mold positioning holes with the machine.
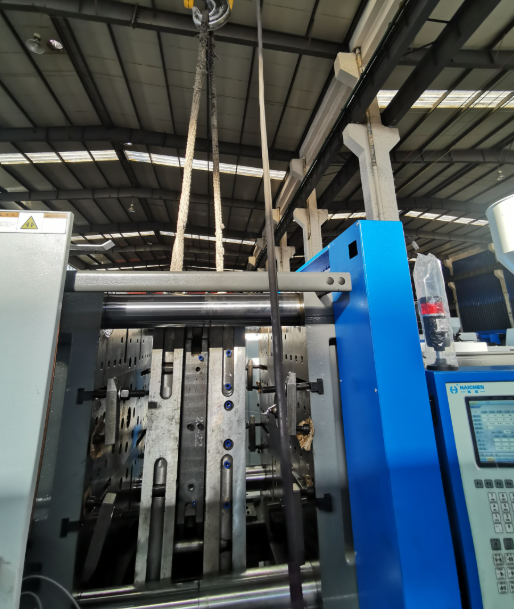
Set the Haichen HCK310 to manual mode and open the mold to full stroke with a level workbench.
Lift the mold steadily with lifting equipment, align the fixed mold with the machine’s fixed platen, and fasten it preliminarily with pressure plates and bolts.
Calibrate the moving mold position to align the machine nozzle center with the mold sprue, with a maximum deviation within 0.2 mm.
Heat the machine barrel to no less than 200℃ and adjust the nozzle to the mold surface level during calibration.
Fully tighten the fixing bolts and check the mold’s opening/closing and demolding system for smooth operation without jamming.
After installation, connect the mold cooling system to the machine’s cooling water circuit for even mold cooling during injection.
Use connecting straps to secure the mold halves and prevent separation during hoisting.
Plastic Injection Molding Machine Trial & Optimization
- Crate Mould preheating
- Clamp
- Injection&hold
Crate Mould preheating
We start trial runs with mold preheating. It greatly lifts product quality and cuts down defects.
The purpose of mold preheating is to eliminate the temperature difference between the mold and the PP melt.
Avoid defects such as cold slug, shrinkage, and deformation caused by uneven cooling of the melt.
And at the same time, reduce the wear of the mold and the machine.
We keep preheating temperature at 60-80℃ for PP fruit crate molds.
This is set through the temperature control system of the Haichen HCK310 injection molding machine.
The preheating time is 30-60 minutes, depending on the mold size and ambient temperature.
Then monitor mold temperatures in real time for even preheating.
The Haichen HCK310 carries a high-precision temperature control system.
This can accurately control the mold preheating temperature, ensuring that the mold reaches the required temperature before injection.
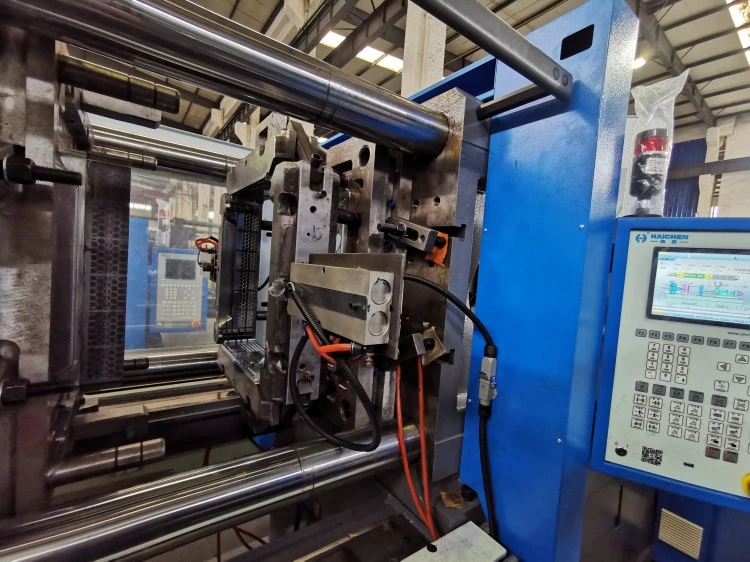
Clamp
The clamping link is to ensure that the mold is tightly closed during injection.
Prevent the PP melt from overflowing (flashing) under high pressure, and ensure the dimensional accuracy of the product.
Then Operate clamping via the Haichen HCK310 clamping system.
Set clamping force by product size, wall thickness, and material.
Then Set 2500-2800kN clamping force for the PP fruit crate.
Adopt a medium clamping speed to protect the mold and the machine.
Then Check the tight mold closure throughout the clamping process.
Inspect the mold position and even stress on the machine tie rods.
The Haichen HCK310 has a clamping force monitoring system.
This can real-time monitor the clamping force and alarm in case of abnormal conditions, avoiding mold damage and product defects.
Injection&hold
All in all Injection and pressure holding are the core links of the injection molding trial run.
Because these directly determine the filling quality and dimensional stability of the product.
The Haichen HCK310 machine adopts a double-rod injection structure.
This makes the injection more stable, and the high-precision linear guide rail reduces the load of the storage and ensures stable back pressure (set to 5-10MPa).
During the injection process, it is necessary to observe the filling state of the melt in the cavity in real time.
We may raise the injection pressure and speed for insufficient filling.
Then we adjust pressure, clamping force, or check mold gaps to fix flash.
The Haichen HCK310 features a built-in parameter memory function.
Which can record the optimized parameters for subsequent mass production.
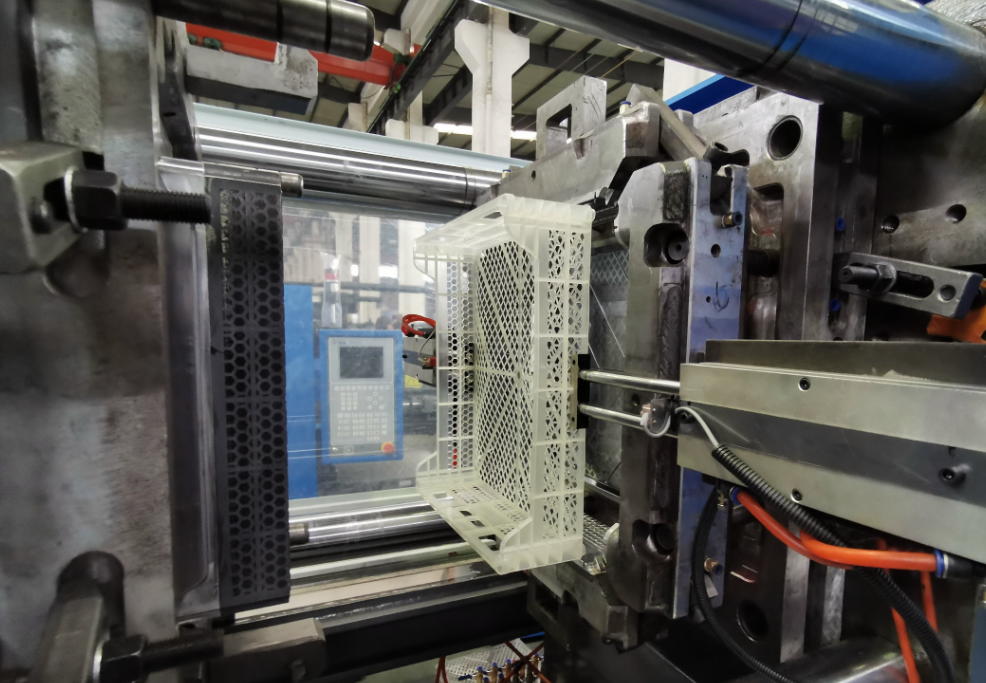
Final inspection
- check dimensions
- check weight
- check performance
Dimensional Precision Check
At Haichen, we use vernier calipers, tape measures, and other professional tools to check key dimensions of the fruit crate: length 400mm, width 450mm, height 120mm, wall thickness, and other core parameters.
Basically we keep the dimensional tolerance within ±0.5mm.
Besides, we also check the flatness and perpendicularity of the products.
This ensures the crates stack steadily and perform well in fruit packaging and logistics transport.
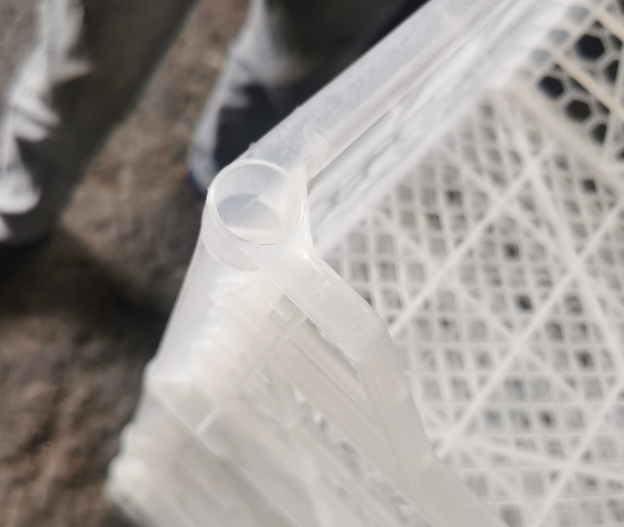
Weight & Cost Control Check
We randomly pick 10 to 20 finished products for weighing control eventually.
The standard average weight is set at 340g, with a permissible tolerance of ±5g.
If the product weight goes beyond the limit in any case.
Whereas we will check whether the mold honeycomb structure is properly designed.
Or adjust the injection molding parameters to cut down raw material consumption.
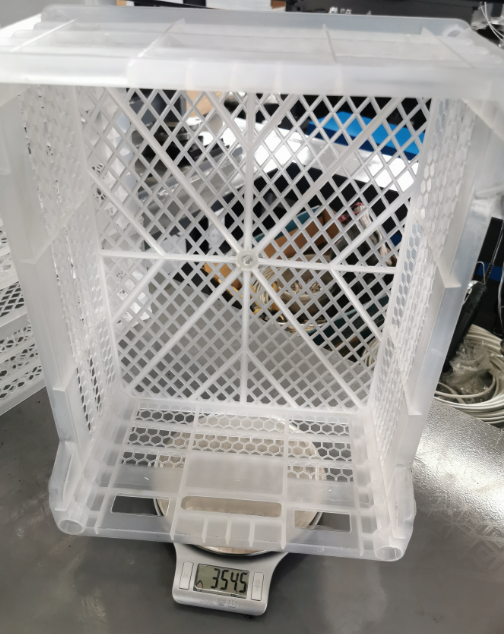
Appearance & Practical Performance Check
We check if the crate surface is smooth, with no burrs, flash, bubbles, sink marks, or warpage.
We also verify the integrity of the honeycomb outer structure and its air permeability.
Then,to fit the size and shape of cherries, apricots, and other fruits.
Meanwhile, we inspect the reinforcing ribs to ensure the bearing capacity meets our design standard without deformation under load.
Whenever we find unqualified products in inspection, our team will analyze the root cause in time.
Significantly,We adjust the mold structure or fine-tune the parameters of our Haichen HCK310 machine, including clamping force, injection pressure, and mold temperature.
Then we do another trial run until all products reach the qualified standard.
Once the final inspection passes, we lock the mold structure and injection parameters and officially start mass production.
If You Are Looking For A Production Line For Plastic Crates
To sum up, developing the injection mold for the 400×450×120mm PP fruit crate and completing a successful trial run on our Haichen HCK310 plastic injection molding machine covers a complete set of standard procedures: mold structure design, mold processing and manufacturing, equipment selection, mold installation, trial run optimization, and finished product inspection.
Then at every stage, we at Haichen fully combine product features, PP material properties, and the inherent performance advantages of our injection molding machines.
So We strictly follow all operational guidelines, especially in raw material saving, mold-machine matching, and product quality control.
Therefore this ensures stable, continuous production, effectively lowers overall production costs, and greatly improves the cost performance of disposable fruit crates.