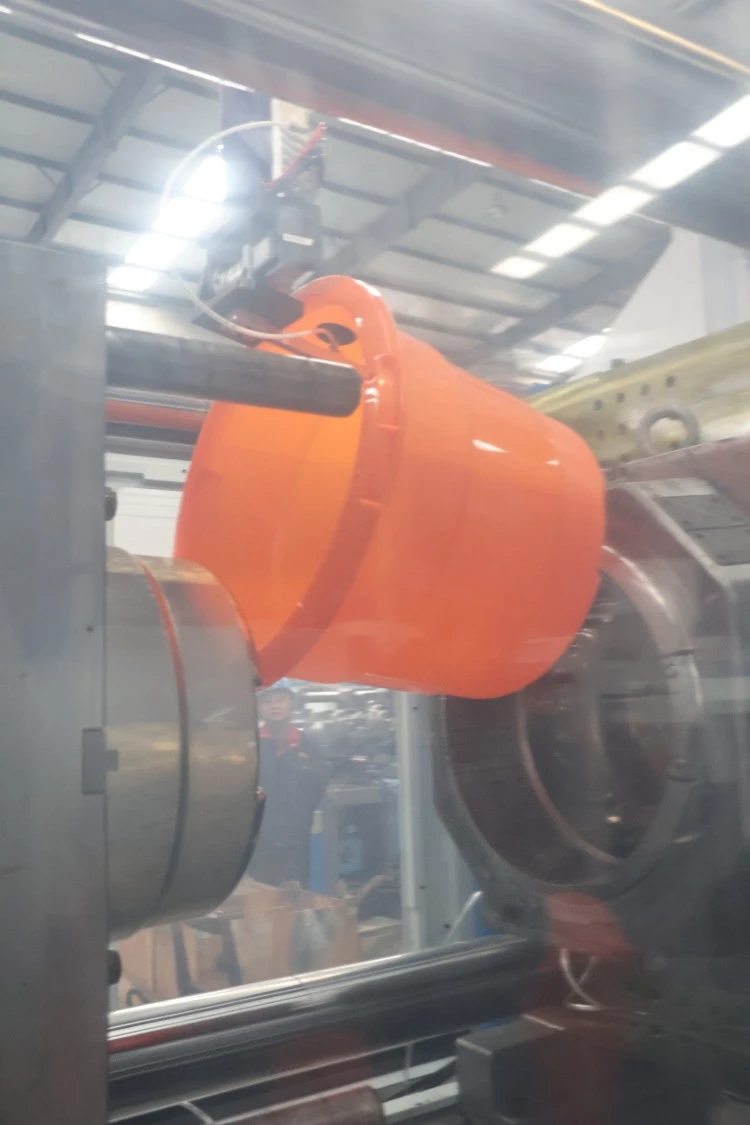
A 5 gallon plastic bucket is made by plastic injection molding machine, through melting plastic material and injects into a mold to form a plastic bucket.
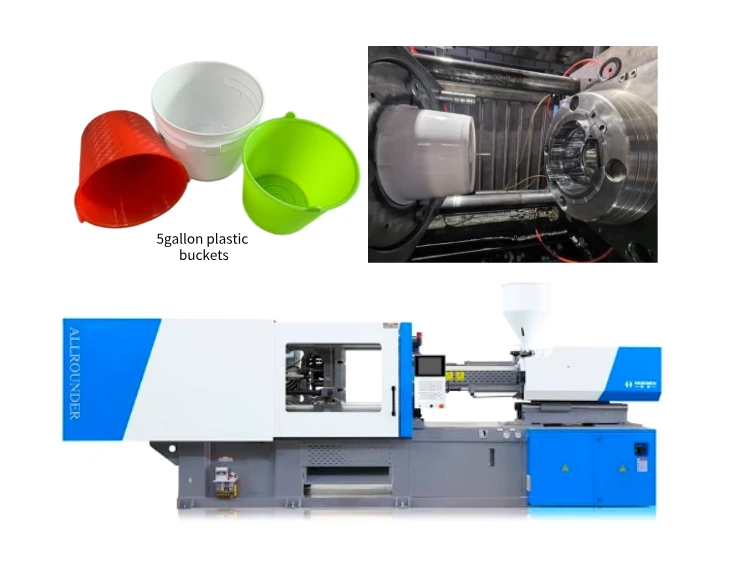
The 5 gallon plastic bucket injection molding work follows five main steps:
- The plastic bucket injection molding machine melts plastic material into liquid form
- The machine clamping unit closes and holds the mold shut
- Injection unit pushes melted material into the 5 gallon bucket mold cavity
- Cools and harden the mold
- The mold opens and ejector pins push the finished 5 gallon bucket out.
On the market, there are many different types of plastic buckets and different manufacturing processes. A 5 gallon plastic water bucket is a large product with thick walls. The injection molding process handles this size well because it uses high clamping force and precise temperature control. Typical 5 gallon buckets weigh 598g to 750g and need a 400 to 700 ton injection molding machine . The main raw materials used for injection plastic bucket manufacturing choice affects cycle time. For example, HDPE buckets cool faster than PET preforms for blow molding.
Four factors affects plastic water buckets production quality and speed: The material type sets the melting temperature. The mold design controls cooling uniformity. Machine parameters like injection speed affect fill quality. Auxiliary equipment like robots and chillers improve cycle time. Haichen , as one of the Chinese plastic bucket injection molding machine manufacturer has over ten years of experience optimizing these factors for 5 gallon plastic bucket production.
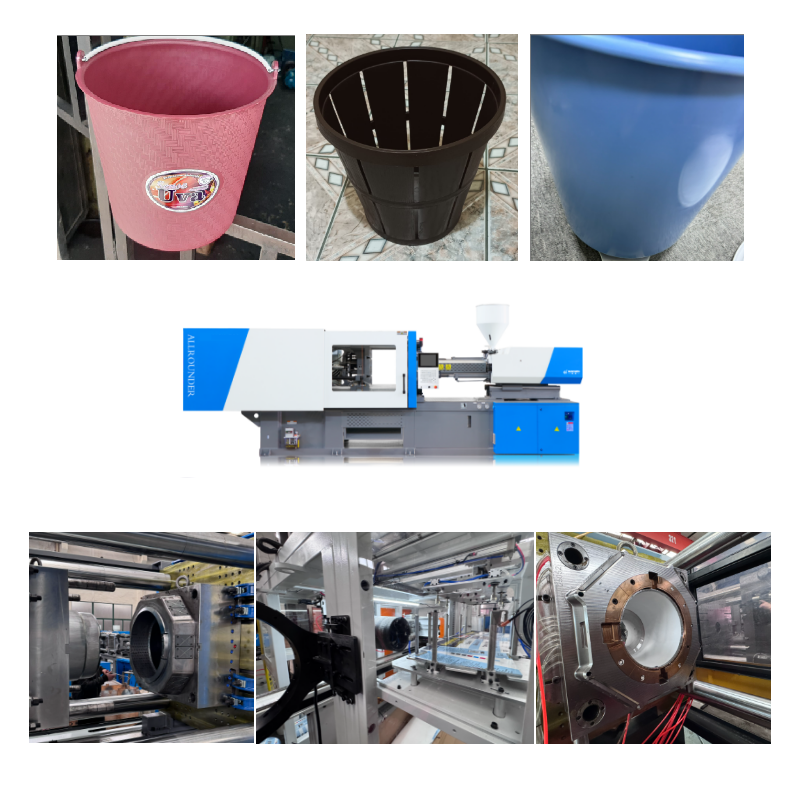
Step1-Melting Material for 5 Gallon Plastic Buckets
-
Material types for water buckets
-
Heating process in the barrel
-
Screw action and melting
Material types for plastic buckets
Manufacturers use HDPE or PP for 5 gallon buckets. HDPE is stronger and more rigid, so it suits heavy-duty water buckets. PP offers good impact resistance for standard applications. For PET water bottles, the process uses a preform mold first, then blow molding . For injection molded buckets, HDPE is the most common choice.
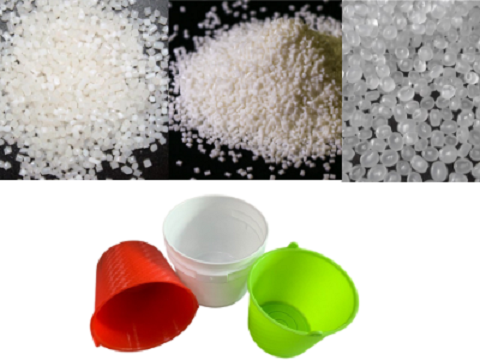
Heating process in the barrel
The plastic bucket injection molding machine feeds plastic pellets from a hopper into a heated barrel. The barrel has several heating zones. The first zone warms the pellets. The middle zones melt them completely. The front zone keeps the plastic at injection temperature. For HDPE, temperatures range from 230°C to 260°C.
Screw action and melting
A screw rotates inside the barrel. This rotation pushes the plastic forward. The screw design creates friction, and this friction adds more heat to the plastic. The melted plastic collects at the front of the barrel. For a 5 gallon bucket weighing 600g, the shot size needs about 700g of melted plastic to account for the runner system.
Haichen uses a special barrier screw for HDPE material. Because the different main raw materials used for injection plastic bucket manufacturing will affect the production quality. This screw design creates consistent melting and prevents unmelted particles. This screw geometry reduces melt temperature variation to within ±2°C.
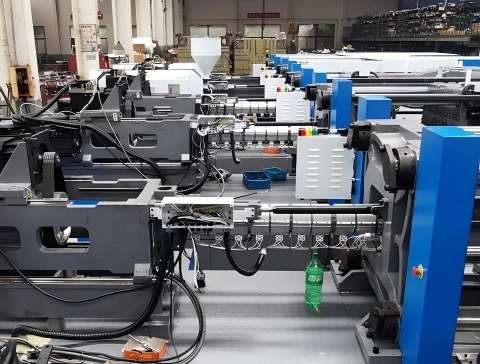
STEP2-5 gallon plastic bucket Closing and Clamping
-
Mold closing motion
-
Clamping force requirements
-
Machine clamping system features
Mold closing motion
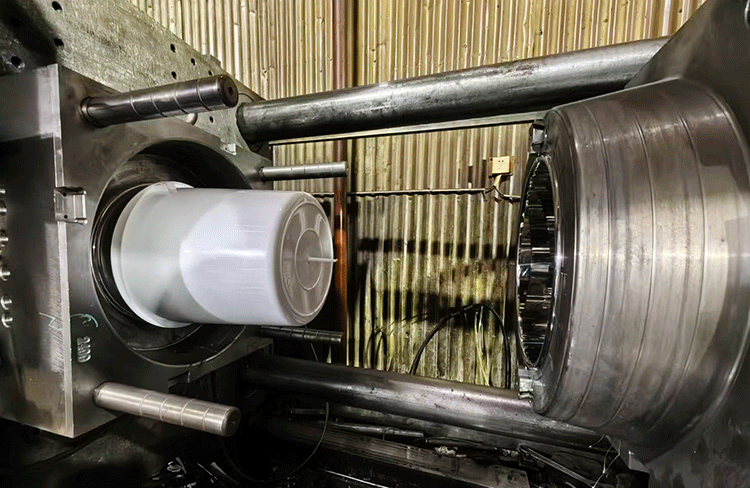
The clamping unit moves the moving platen toward the fixed platen. This action closes the two mold halves together. For a 5 gallon bucket mold, the machine first uses low pressure to close. It then increases speed to complete the closing motion. The mold must seal tightly to prevent leaks.
Clamping force requirements
A 5 gallon bucket needs high clamping force because the plastic enters under high pressure. For a bucket with a projected area of about 2000 cm², the required force is 400 to 700 tons. Too little force causes the mold to open slightly. This creates a defect called flash on the bucket rim.
Machine Clamping system features
Haichen , one of Chinese plastic bucket injection molding machine manufacturer use a five-point toggle clamping system injection machine. This design provides stable force distribution across the mold. The system also reduces energy use by 30% compared to hydraulic clamping. For 5 gallon bucket production, Haichen’s clamping system maintains consistent force throughout the injection and cooling stages.
We also know the problems and solutions in the production of plastic buckets so can supply better service for you.
| Haichen HCK310 PLASTIC INJECTION MOLDING MACHINE | ||||
| INJECTION UNIT | ||||
| ITEM | UNIT | A | B | C |
| INJECTION UNIT | ||||
| Screw diameter | mm | 60 | 65 | 70 |
| Screw L/D ratio | L/D | 23.8 | 22.0 | 20.4 |
| Shot volume(theoretical) | cm3 | 919 | 1078 | 1251 |
| Injiection weight(ps) | g | 836 | 981 | 1138 |
| oz | 29.5 | 34.6 | 40.1 | |
| Injection pressure | Bar | 2078 | 1771 | 1527 |
| Injection rate | cm3/s | 309 | 362 | 420 |
| Plasticizing capacity | g/s | 42 | 51 | 60 |
| Screw speed (Max.) | r/min | 210 | ||
| CLAMPING UNIT | ||||
| Clamping force | Kn | 3100 | ||
| Space between tie bars(W×H) | mm | 670×620 | ||
| Platens size | mm | 950×900 | ||
| Opening stroke | mm | 610 | ||
| Min.Mold height | mm | 270 | ||
| Max.Mold height | mm | 670 | ||
| Distance between platens(daylight) | mm | 1280 | ||
| Ejector stroke | mm | 170 | ||
| Ejector force | Kn | 90 | ||
| OTHERS | ||||
| Systerm pressure | Bar | 175 | ||
| Pump motor | Kw | 41 | ||
| Heating power | Kw | 26.0 | ||
| Oiltank cubage | L | 400 | ||
| Machine dimension(L×W×H) | m | 6.5×1.6×2.1 | ||
| Machine weight | t | 10.3 | ||
injection of 5 Gallon plastic bucket
-
Injection speed and pressure
-
Plastic flow through the mold
-
Injection control technology
Injection speed and pressure
The screw moves forward like a plunger. This action pushes melted plastic through a nozzle into the mold. For a 5 gallon water bucket, injection takes 2 to 4 seconds. The pressure ranges from 80 to 150 MPa. Too much speed causes air traps. Too little speed causes incomplete filling.
Plastic flow through the mold
The melted plastic first enters the sprue, which is the main channel. It then flows through runners to reach the cavity. The gate is the small opening where plastic enters the bucket shape. For a 5 gallon water bucket, a single large gate at the bottom center works best. This gate location ensures even flow to all side walls during plastic bucket injection molding.
Injection control technology
Haichen machines use closed-loop servo control for injection speed. This system maintains the set speed within 0.1 second response time. The multi-stage injection profile allows operators to set different speeds for different fill stages. For 5 gallon buckets, Haichen recommends a three-stage injection profile. Slow speed for the first 10%, medium for the next 60%, and fast for the final 30%.
Cooling and Solidification Of 5 gallon plastic bucket
-
Cooling channels in the mold
-
Cooling time for thick walls
-
Optimize cooling
Cooling channels in the mold
The mold has cooling channels built inside it. Cool water flows through these channels at 7°C to 30°C. This removes heat from the melted plastic. The bucket hardens from the outside inward. Good cooling channel design prevents warping.
Cooling time for thick walls
A 5 gallon bucket has thick walls, so cooling takes longer than small products. Typical cooling time is 10 to 25 seconds. This is the longest part of the production cycle. Using a chiller with precise temperature control reduces cycle time. Shorter cooling means more buckets per hour.
Optimize Cooling
Haichen provides mold cooling analysis for each customer’s bucket design. We calculate the optimal cooling channel layout and water flow rate. Our HCK series machines also feature a dedicated cooling circuit control. This allows operators to adjust cooling time in 0.1 second increments. For a standard 5 gallon bucket, Haichen’s optimization reduces cooling time by 15-20%.
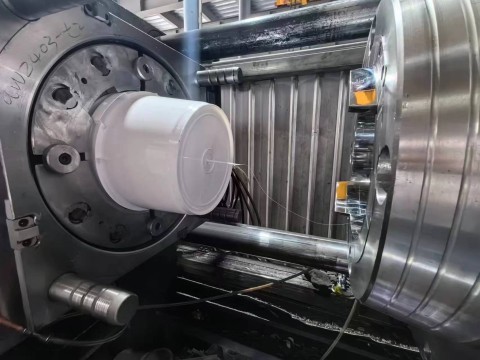
Ejection and Demoulding of 5 gallon plastic bucket
-
Ejector pin operation
-
Robot removal options
-
Design ejection system
Ejector pin operation
After the plastic hardens, the machine opens the mold. Ejector pins then push the bucket off the mold surface. For large buckets, molds use multiple ejector pins for even force distribution. The bucket then falls onto a conveyor or is removed by a robot arm.
Robot removal options
For automated production, a robot removes the finished bucket. This speeds up the cycle and prevents damage. The robot can also place in-mold labels (IML) before injection. For 5 gallon buckets, a side-entry robot works best because it does not interfere with the operator side.
Design ejection system
The ejector force ranges from 5 to 15 tons depending on machine model. The stroke length is adjustable from 50mm to 200mm. For 5 gallon buckets, Haichen recommends a 150mm ejector stroke to fully clear the bucket from the core side. The system also includes an ejector plate return function for mold safety. Haichen machines use a hydraulic ejector system with adjustable force and stroke.