
Injection molding temperature setting range: 150-340 °C for the barrel(melting temperature), 200-280°C for the nozzle, and 10-150°C for the mold. The injection Molding Machine Temperature setting depends on the plastic resin used. Materials like PP and ABS use 200-260°C (barrel), while materials such as PEEK or LCP require higher settings, 300-400°C (barrel).
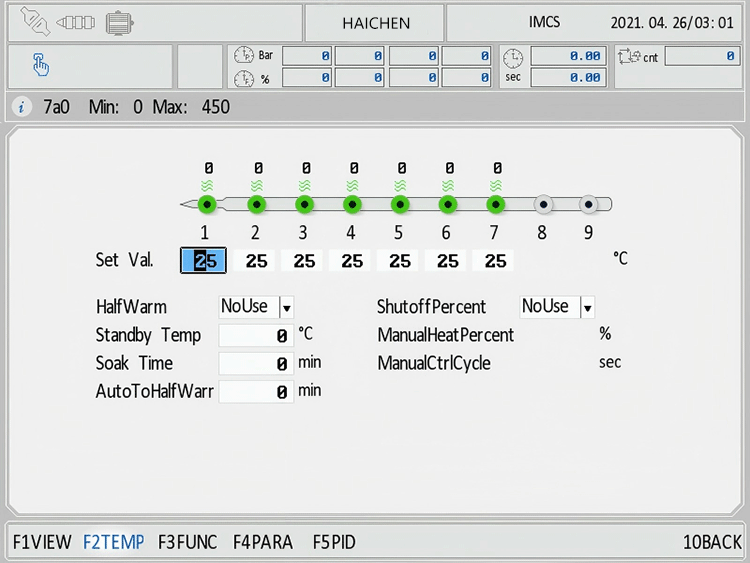
To set the temperature on an injection molding machine, you need to adjust three main parts: the barrel, the nozzle, and the mold.
- First, set the barrel to the melting temperature of your plastic (usually between 150°C and 400°C).
- Second, set the nozzle about 5-10°C lower than the front barrel zone.
- Third, set the mold temperature based on your plastic type (usually 20°C to 120°C).
Always check the material data sheet before you start. Then run a few test parts and make small changes until the parts look good.
| Item | Marterial | Barrel temperature(℃) | Material temperature(℃) | Mold temperature(℃) |
| 1 | PE | 160-220 | 180-200 | 20-60 |
| 2 | PP | 190-260 | 210-230 | 20-80 |
| 3 | PVC | 160-200 | 170-190 | 20-60 |
| 4 | PS | 180-240 | 200-220 | 20-70 |
| 5 | HIPS | 190-250 | 210-230 | 20-70 |
| 6 | ABS | 200-260 | 220-240 | 40-80 |
| 7 | POM | 190-230 | 200-220 | 60-100 |
| 8 | PA6 | 220-280 | 240-260 | 60-120 |
| 9 | PA66 | 240-300 | 260-280 | 80-120 |
| 10 | PC | 260-320 | 280-300 | 80-120 |
| 11 | PMMA | 200-260 | 220-240 | 40-80 |
| 12 | PPO | 260-320 | 280-300 | 80-120 |
| 13 | PPS | 280-340 | 300-320 | 100-150 |
| 14 | PEEK | 350-400 | 370-390 | 120-160 |
| 15 | PTFE | 320-380 | 340-360 | 80-120 |
| 16 | TPU | 210-250 | 220-240 | 40-80 |
| 17 | TPE/TPEE | 180-250 | 200-220 | 20-60 |
| 18 | PLA | 180-220 | 190-210 | 20-60 |
| 19 | LCP | 300-360 | 320-340 | 100-150 |
| 20 | ETFE | 260-320 | 280-300 | 60-100 |
What is the injection Molding Machine Temperature setting?
Temperature setting means choosing the right heat for different parts of the injection molding machine. Good temperature control helps melt the plastic evenly. It also helps the plastic flow well into the mold and cool down at the right speed. When you set the temperature correctly, your parts will have fewer defects and better quality.
1. Barrel Temperature setting
What It Is
The barrel is the long tube where the plastic melts on the injection molding machine. Most machines divide the barrel into three or four zones. Each zone has its own temperature setting.
Plastic needs different heat levels as it moves through the barrel. The first zone starts melting the plastic. The middle zones mix it well. The last zone gets it ready for injection. If a zone is too cold, the plastic may not melt fully. If a zone is too hot, the plastic may burn.
How to Set It
For most plastics, the barrel temperature is between 150°C and 300°C. Here are some common examples:
| Plastic Type | Barrel Temperature (°C) |
| ABS | 200 – 240 |
| PP | 220 – 250 |
| HDPE | 200 – 260 |
| PC | 280 – 320 |
| POM | 160 – 280 |
Always start from the middle of the range. Then adjust based on your part quality.
2. Nozzle Temperature setting
What It Is
The nozzle sits at the end of the barrel. It directs the melted plastic into the mold. The nozzle has its own heater. It is the last step on the injection Molding Machine Temperature setting.
The nozzle temperature keeps the plastic from cooling down before it enters the mold. If the nozzle is too cold, the plastic will not flow easily. You may get short shots or flow marks. If the nozzle is too hot, the plastic may drip out between cycles. This is called drooling.
How to Set It
Set the nozzle temperature slightly lower than the front barrel zone. Usually, it is 5°C to 10°C cooler than the last range of barrel. For most materials, the nozzle temperature is between 200°C and 280°C.
3. Mold Temperature setting
What It Is
Mold temperature is the heat level of the mold itself. The mold does not have heaters by itself. It uses a cooling system or heating system to control its temperature.
The mold temperature controls how fast the part cools. A colder mold cools the part faster but may cause surface defects. A hotter mold gives a better surface finish but takes more time. The right mold temperature gives you good quality and short cycle times.
How to Set It
Mold temperature usually falls between 20°C and 120°C. Here are some examples:
| Plastic Type | Mold Temperature (°C) |
| PP | 30 – 60 |
| ABS | 60 – 80 |
| PC | 80 – 100 |
| PA6 | 60 – 90 |
| POM | 10 – 80 |
Use a mold temperature controller or a water chiller to keep the mold stable.
4. Heating Band Temperature setting
What It Is
Heating bands are ring-shaped heaters wrapped around the barrel. The injection Molding Machine Temperature setting actually is the same as the heating band temperature setting.
The heating band is fixed on the barrel, so the setting of these two parts is the same. No difference.
They give extra heat to specific zones. Heating bands help keep the barrel temperature stable. Without them, the barrel may lose heat to the air. This is especially important when you use high-temperature plastics like PC or PEEK.
How to Set It
Set the heating bands to the same target as each barrel zone. The control system will turn them on and off to hold the correct temperature. Most heating bands work in the range of 200°C to 250°C.
5. Cooling System Temperature setting
What It Is
The cooling system uses water or oil to remove heat from the mold. It helps the part cool down and harden.
Good cooling stops the part from warping or shrinking too much. It also shortens the time you wait before opening the mold. Poor cooling can cause longer cycles and bad parts.
How to Set It
The cooling water temperature is usually between 15°C and 25°C. For high-temperature molds, you may need water up to 80°C. Use a chiller or a cooling tower to control the water temperature.


