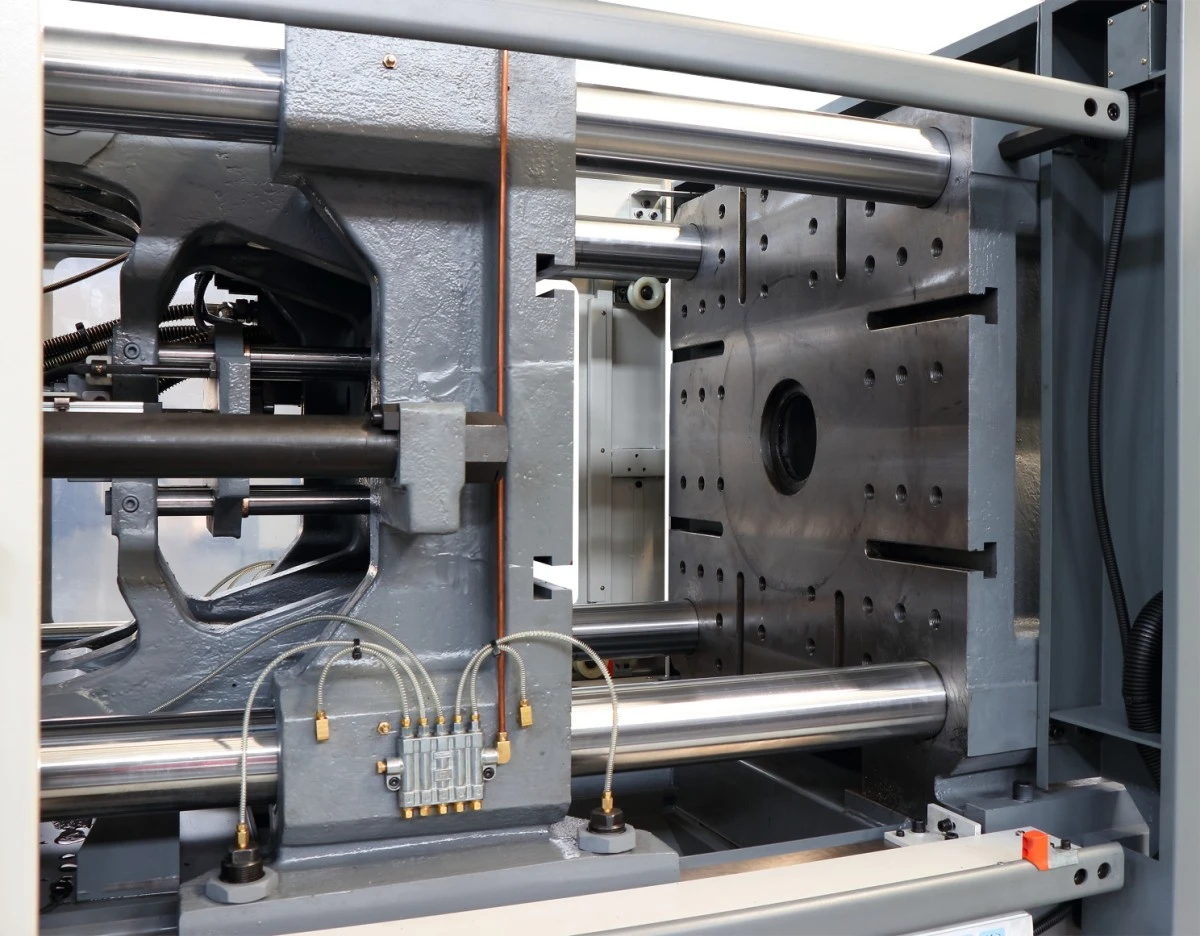
PET Jars Injection Molding Problems are blurry surface,unstable dimension,cracks and poor toughness,solutions are adjust the parameters of the injection molding machine,adjust the mould,add auxiliary equipment.
PET Jars are widely used for food, cosmetic and daily product packaging, so stable molding quality is very important for product sales and safety.
This article sorts out these typical molding problems and shares practical solutions for PET Jars production, to help manufacturers make more qualified and stable PET Jars.
First of all, minor defects are pretty normal in PET Jars mass injection molding due to long-time machine operation and repeated mold use.
In addition, these small flaws can easily ruin the appearance and shorten the service life of finished PET Jars, and even lead to large batch of unqualified products.
Finally, adopting targeted solutions can effectively cut production waste and raise the overall product yield, which also helps factories save more production cost.
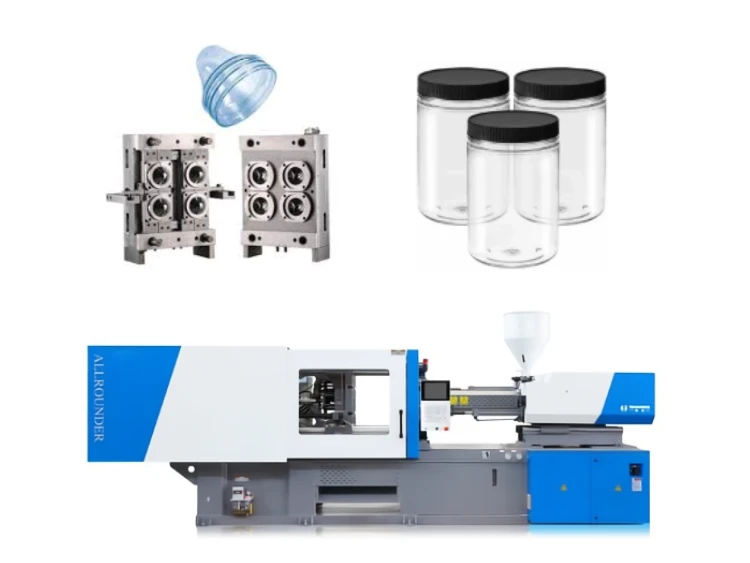
Problem 1:PET Jars Blurry Surface
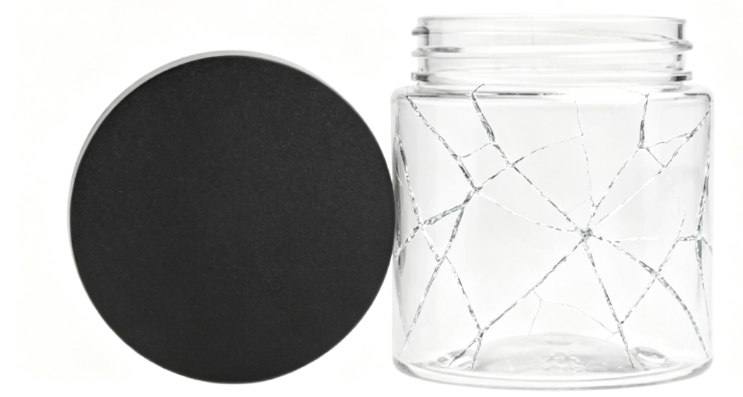
First, blurry and hazy surfaces are the most frequent issue for finished PET Jars. Specifically, over-crystallization of PET materials will lower the transparency of PET Jars.
Meanwhile, leftover moisture in raw materials and inconsistent cooling speed can also cause foggy surfaces.
Furthermore, fine impurities mixed in PET raw materials are another common cause of persistent haze on PET Jars.
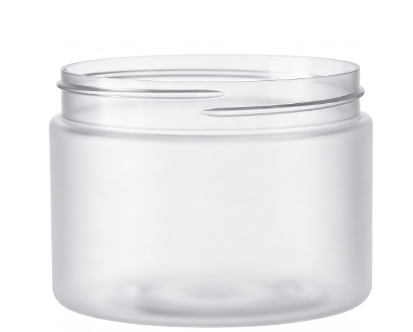
Problem 2:PET Jars Unstable Dimension
Secondly, PET Jars often have inconsistent sizes in mass production. For example, uneven melt temperature leads to different shrinkage levels of PET materials.
Besides, unstable holding pressure and irregular injection cycle time will result in different height and wall thickness among PET Jars.
Thus, this common issue makes finished PET Jars hard to assemble with consistent quality.
Problem 3:PET Jars Cracks and Poor Toughness
Thirdly, PET Jars may develop tiny cracks and turn brittle after injection molding. To be specific, incomplete drying of raw materials makes PET Jars lose basic toughness.
In addition, excessive heating during melting will damage the internal structure of PET materials. As a result, finished PET Jars are easy to crack during daily packaging and transportation.
Solution 1:Adjust machine parameters To solve Blurry Surface
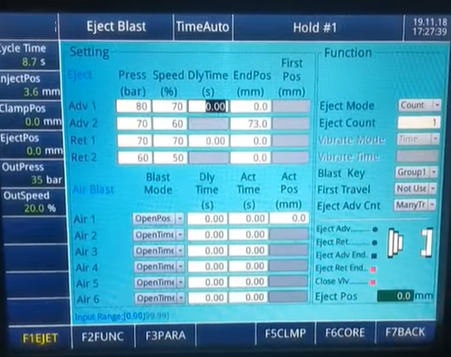
First, improper injection machine running parameters are the core cause of hazy and blurry PET Jars surfaces. To fix this issue, we mainly adjust machine temperature, speed and pressure settings strictly based on standard PET molding rules. First, set a reasonable barrel segmented temperature between 240℃ and 280℃, and keep tiny temperature fluctuations within ±3℃ to avoid local overheating.
In addition, lower screw rotating speed and back pressure to reduce excessive shear heat, which prevents PET material over-crystallization and molecular degradation. Moreover, control injection speed at a moderate level, since fast injection easily causes uneven melt flow and surface fogging. In this way, stable machine parameters greatly improve the surface transparency of PET Jars in daily production.
Solution 2:Adjust the mould To solve Unstable Dimension
Secondly, unreasonable mold design and poor mold maintenance directly lead to unstable sizes of PET Jars. Different from machine adjustment, this solution focuses entirely on mold structure and transformation.
First, optimize the mold gate size and position to make PET melt fill the cavity evenly without dead corners.
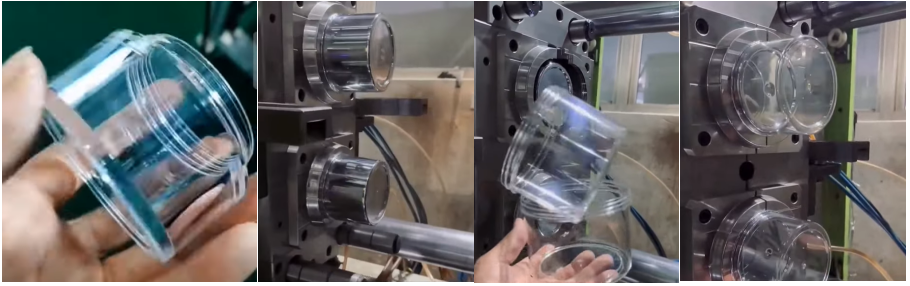
Meanwhile, improve mold venting slots to release internal air smoothly and avoid uneven shrinkage. Besides, adjust and fix mold clamping force to prevent slight mold opening during injection. Furthermore, polish mold cavities regularly to ensure smooth material filling and consistent cooling effects. These targeted mold upgrades effectively unify the wall thickness and height of batch-produced PET Jars.
Solution 3:Add auxiliary equipment To solve Cracks and Poor Toughness
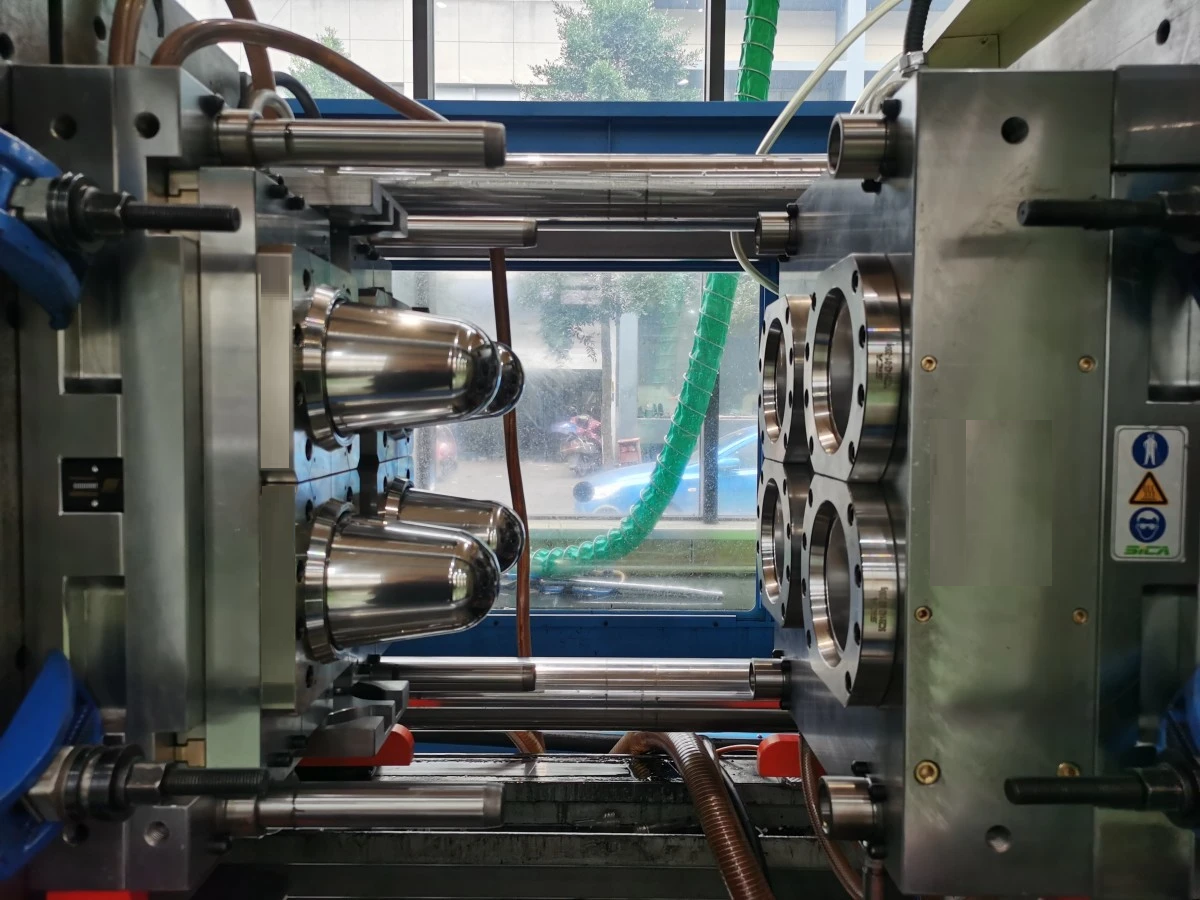
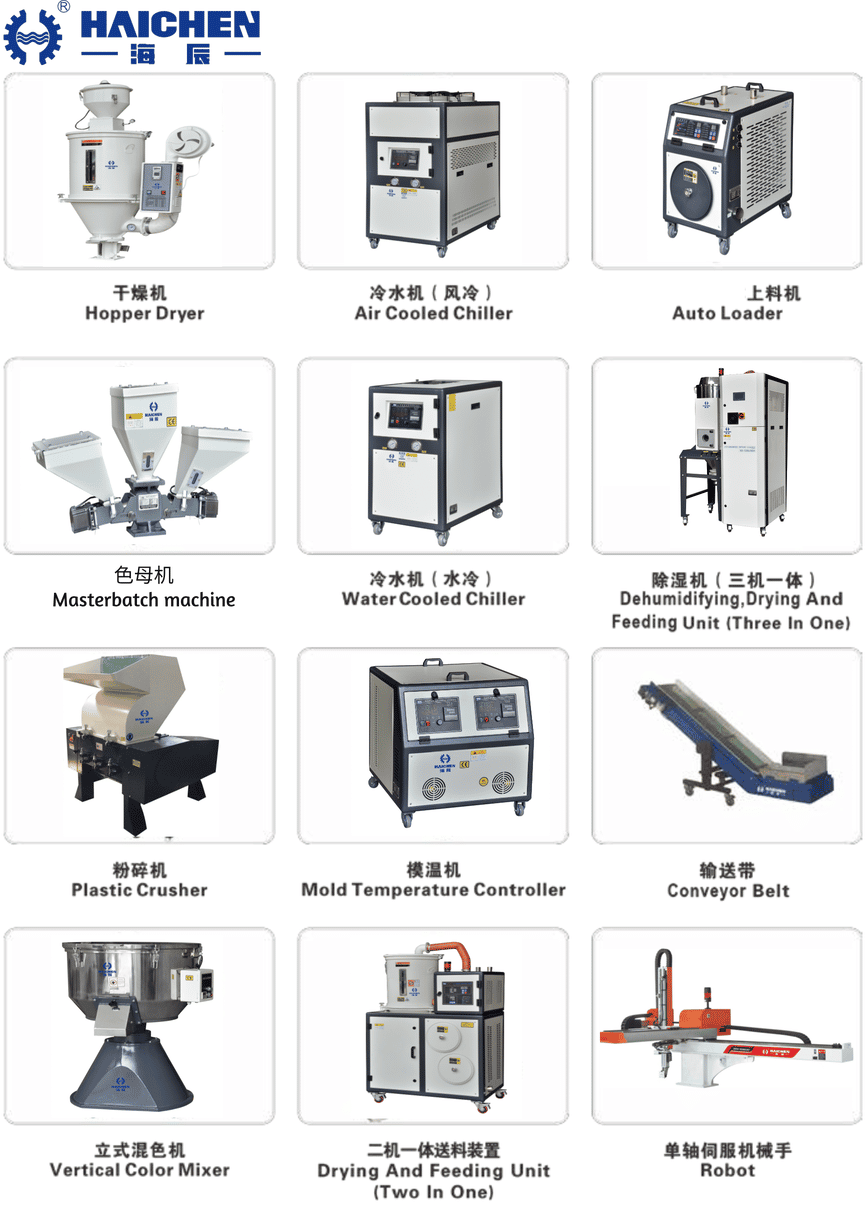
Thirdly, unstandardized use of auxiliary equipment is the main hidden cause of cracks and poor toughness on PET Jars. Common auxiliary devices include material dryers and cooling chillers.
First, set the dryer to standard temperature and time to fully remove residual moisture in PET raw materials, which avoids brittle finished products.
In addition, stabilize the chiller operation to keep uniform mold cooling speed, so PET Jars will not produce internal stress and tiny cracks due to fast or uneven cooling.
Moreover, regularly check auxiliary equipment pipelines to prevent blockage and unstable operation. These auxiliary equipment adjustments perfectly make up for machine and mold blind spots and greatly improve the overall quality of PET Jars.
Is it possible to avoid these PET Jars problems in advance?
- Standard operation
- Regular inspection and maintenance
Standard operation
First, machine manufacturers suggest customers follow fixed start-up steps for all PET Jars production. Before formal mass production, operators need to preheat the machine barrel step by step instead of rapid heating.
This slow preheating method avoids local overheating and prevents PET material crystallization and surface haze.
In addition, we recommend customers save a dedicated PET molding parameter group in the machine system. The preset temperature, injection speed and holding pressure can serve as the standard baseline.
When customers adjust parameters, they only make tiny changes based on the fixed data.
This operation effectively avoids unstable dimension caused by random parameter modification.
Besides, we remind customers to match machine parameters with PET material grades. Different raw materials need slight parameter fine-tuning to prevent material decomposition and brittle cracks.
Regular inspection and maintenance
Secondly, machine manufacturers set clear daily and weekly maintenance standards for customer use.
On adaily basis, operators need to check the screw and nozzle condition before starting the machine.
Residualdegraded materials will cause surface impurities and tiny cracks on PET Jars, so timely cleaning is necessary.
Every week, customers need to inspect machine pressure systems and cooling circulation systems.
Unstablepressure output leads to uneven product size, while blocked cooling pipelines cause unbalanced heatdissipation. Furthermore, we suggest customers do regular mold matching checks.
Stable mold clampingcoordination ensures uniform melt filing and reduces batch defects. All these standardized maintenance stepsgreatly lower the failure rate of PET Jars injection molding.